Contained Transfer Interfaces: Double O-Ring, Crimp & Heat Weld
Behind every flexible-film containment method — continuous liners, film-connection systems, glove-to-isolator joints, even BIBO filter change — sits a small number of sealing techniques. Get the interface right and the transfer stays closed; get it wrong and potent powder escapes at exactly the wrong moment. This guide covers the three that matter: the double O-ring, the mechanical crimp, and the heat weld.
The double O-ring
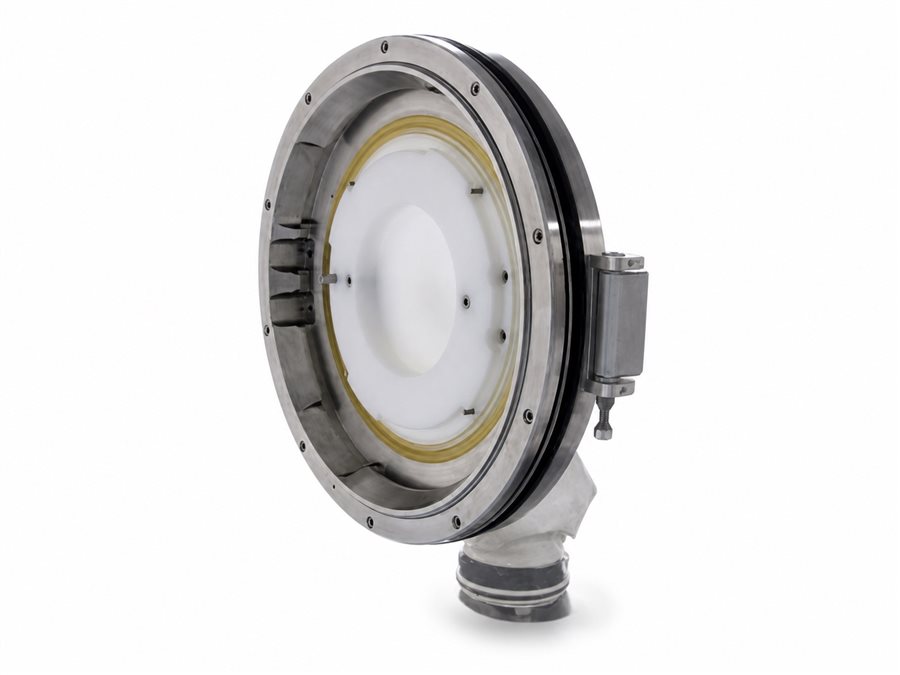
The double O-ring is the basis of many flexible-film transfer seals — continuous-bag systems, film-connection systems, the glove-to-isolator joint, and BIBO filter-change systems. Two rolled film gaskets are sealed with the help of two O-rings onto an adapter fitted to the equipment; mounting the second film layer over the first isolates the adapter and the equipment interior from the room environment.
- Although the O-rings can be held in place with a clamp, their sealing against over-pressure is limited.
- With large-diameter O-rings, assembly is more complex and can be awkward to handle.
- Large-diameter O-rings can also seal less well — especially if the plastic sleeve is oversized and the sealing face has multiple folds.
- The device surface между the two O-rings may become contaminated.
Mechanical film closure (crimp & cut)
The simplest closure is to fit two ties close together around the film sleeve and cut in between, leaving two tied, separated ends. In practice this carries a real exposure risk: material can be released from the contaminated section between the tie and the open end, especially with potent compounds. Taping over the cut ends reduces the risk but complicates the operation. Developments include proprietary tie systems that minimise the distance between the tie heads and clamp the gasket as tightly as possible to trap any powder in the folds; the exposed end should also be capped as soon as possible after cutting. A typical mechanical closure uses two closure folds fixed around the film to be separated, with a film cutter cutting between them — a double-crimp keeps the distance between the two tie heads to a minimum.
- If a tie head loosens during separation, containment fails.
- The bag’s folds must adhere tightly to be effective, and the separated port must be sealed so powder cannot fall out of the crimped folds.
- The distance between folds matters — too large and the opening step risks particle release.
- Crimp heads must have no sharp edges, which could damage the bag in transit.
- Proprietary crimp systems are designed for specific sleeve sizes and materials and may not seal others reliably.
- Shear cutting can produce plastic debris that then contaminates the transferred product.
Heat-weld film closure
A heat-weld system uses two welding jaws that ideally produce a triple weld seam. It only works with polyethylene (PE) film — PU and PVC films need a high-frequency welding system instead. Closing the triple seam at once forms both a sealed base for the filled bag and the base of the new bag. The middle seam can be made wider, with automatic film separation built in to replace manual cutting along the seam and reduce contamination risk. The advantage is that the cut is made inside the weld, with no exposure of material. Conversely, a heavily contaminated surface may not seal effectively, which can cause seal failure and subsequent leakage — so, ideally, heat-seal on a clean film surface.
- If the film is not stretched flat, folds form in the weld and affect the seal.
- Residue on or in the seam causes weld faults.
- The high jaw-surface temperature (typically ~150 °C) may exceed the limits of a hazardous-area or ATEX classification.
- The high temperature can also degrade the product, and heat from chemical exotherms or autoignition can raise safety concerns.
These interfaces are what make a continuous liner и a раздельный клапан-бабочка contained, and they govern safe filter change on a BIBO housing. Match the sealing approach to the compound’s Группа OEB.
Сопутствующие товары
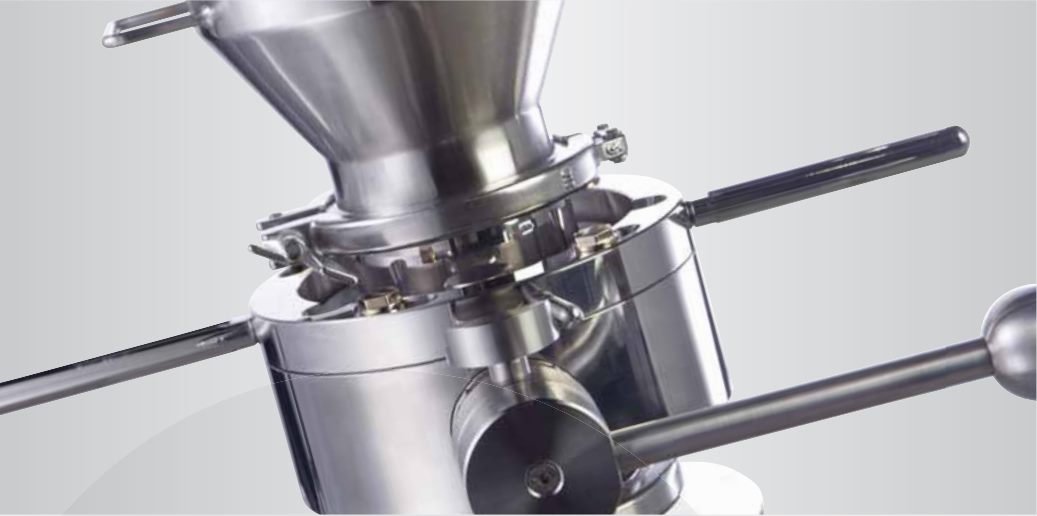 Двухпозиционный клапан типа «бабочка» с альфа-бета-разделениемРазделительный клапан для безопасного и без пыли перекачки мощных порошков.Перемещение и локализация
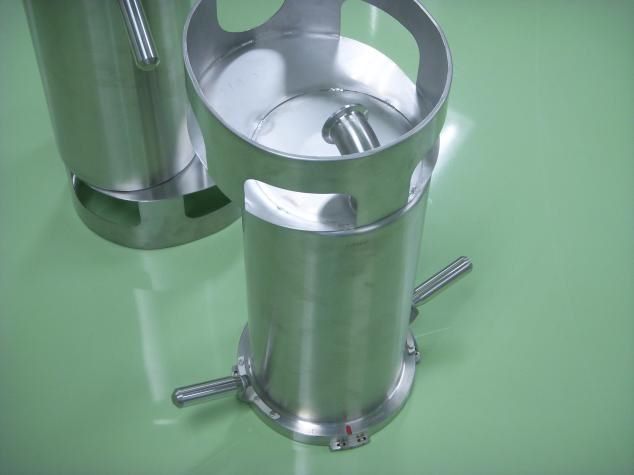 RTP — порт быстрой передачи данныхБыстрый перенос в стерильной среде для переноса в изоляторы.Перемещение и локализация
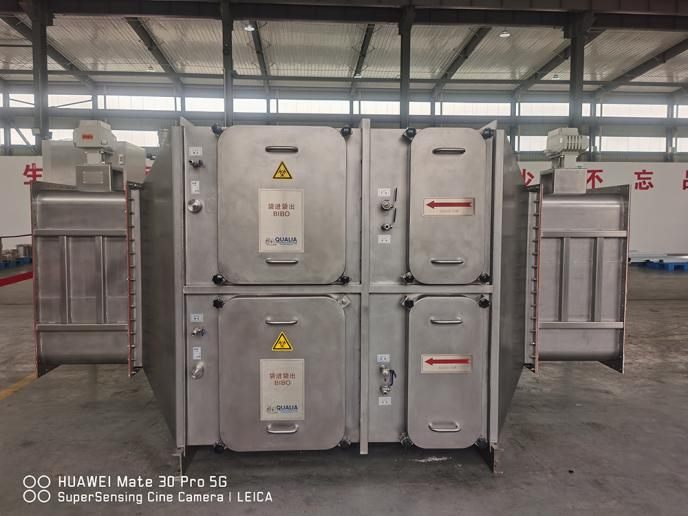 Корпус фильтра BIBOКорпус для фильтрации HEPA для переноса фильтрации из одной упаковки в другую в лабораториях P3/P4.Вентиляционная система
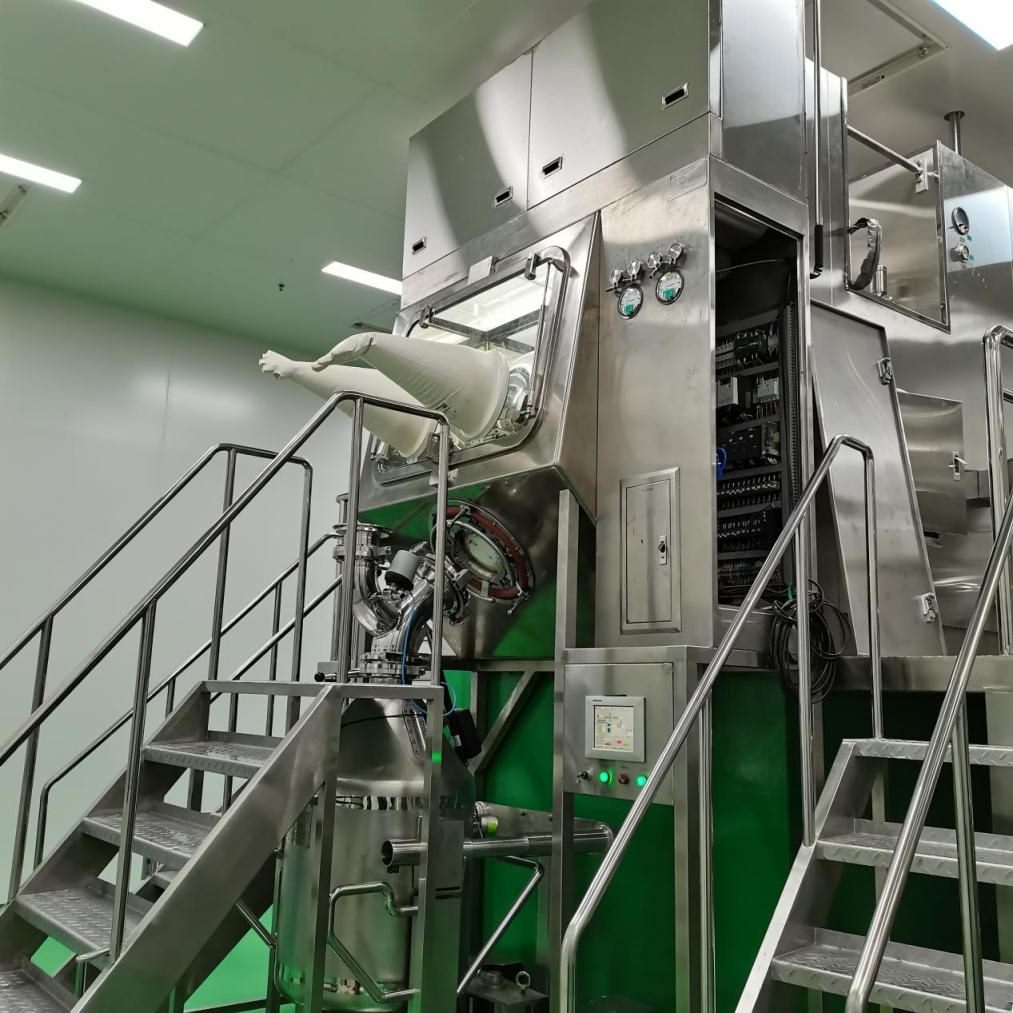 Изолятор для дозирования и удержания (OEB5)Барьер с отрицательным давлением для взвешивания, розлива и отбора проб высокоактивных фармацевтических ингредиентов (HPAPI).Изоляторы и барьеры
Designing a contained transfer interface?
Tell us your film system, compound potency and whether the area is ATEX-classified, and our engineers will recommend the sealing method — O-ring, crimp or weld — that fits.